
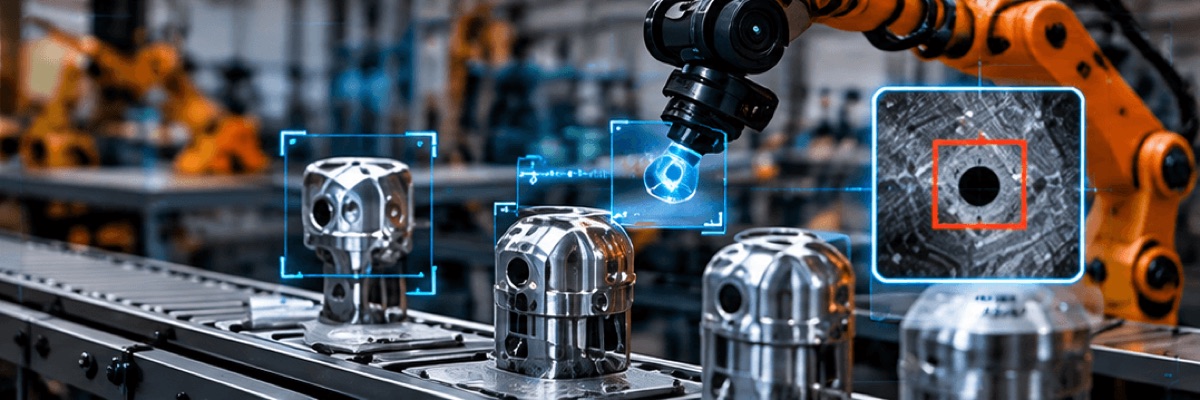
Computer Vision for Quality Control: Detecting Manufacturing Defects with AI
Quality inspection problems suited to vision
Contrast cosmetic defects, missing parts, dimensional errors and assembly mistakes
The useful question is not whether this capability exists in principle, but how the team will validate it under normal and exceptional conditions. Map the current workflow before changing it.
Consider a manufacturer inspecting small surface defects on a moving production line. Instead of judging success by a demonstration, the manufacturing quality team should reproduce realistic cases, record exceptions, and compare the outcome against the current process. The goal is repeatable performance under stated conditions, not a claim that the technique eliminates uncertainty.
Explain when conventional sensors outperform image-based inspection
A reliable approach to when conventional sensors outperform image-based inspection starts by identifying the input, the expected output, and what a person should do if those two do not agree. Map the current workflow before changing it.
For example, with a manufacturer inspecting small surface defects on a moving production line, the first version can be evaluated on a small, representative sample. The manufacturing quality team should keep difficult cases in the test set rather than removing them because they make the results look worse. This reduces the risk of a technically successful pilot that cannot be maintained after launch.
What to do next: The manufacturing quality team should turn this part of the plan into a short written test, with an owner, an expected result, and a reason to revisit the decision. This is especially valuable when a pilot is handed to a separate production team.
Build a reliable image dataset
Cover camera position, illumination, annotations and class imbalance
A reliable approach to cover camera position, illumination, annotations and class imbalance starts by identifying the input, the expected output, and what a person should do if those two do not agree. Map the current workflow before changing it.
For example, with a manufacturer inspecting small surface defects on a moving production line, the first version can be evaluated on a small, representative sample. The manufacturing quality team should keep difficult cases in the test set rather than removing them because they make the results look worse. This reduces the risk of a technically successful pilot that cannot be maintained after launch.
Plan collection of rare defects and changes in production lines
This part of the design deserves more than a configuration checkbox. Its practical value depends on the decision that follows from the result. Map the current workflow before changing it.
Imagine a manufacturer inspecting small surface defects on a moving production line. A pilot should include incomplete information, peak-load conditions, and a clear path back to the existing process. Clear acceptance criteria also make it possible to compare internal development with external tools fairly.
What to do next: The manufacturing quality team should turn this part of the plan into a short written test, with an owner, an expected result, and a reason to revisit the decision. This is especially valuable when a pilot is handed to a separate production team.
Choose and validate the detection approach
Compare classification, object detection and anomaly detection
This part of the design deserves more than a configuration checkbox. Its practical value depends on the decision that follows from the result. Map the current workflow before changing it.
Imagine a manufacturer inspecting small surface defects on a moving production line. A pilot should include incomplete information, peak-load conditions, and a clear path back to the existing process. Clear acceptance criteria also make it possible to compare internal development with external tools fairly.
Measure false rejects, missed defects, precision and recall by defect class
For this requirement, define the situation in which it needs to work, the result that users expect, and the failure that the team intends to prevent. Map the current workflow before changing it.
In the case of a manufacturer inspecting small surface defects on a moving production line, a change may help one group while harming another. The manufacturing quality team needs segmented results and a written acceptance rule. The strongest design makes its limitations visible before they become customer-facing incidents.
What to do next: The manufacturing quality team should turn this part of the plan into a short written test, with an owner, an expected result, and a reason to revisit the decision. This is especially valuable when a pilot is handed to a separate production team.
Deploy inspection into the production line
Discuss edge processing, inference speed, PLC/MES integration and operator overrides
For this requirement, define the situation in which it needs to work, the result that users expect, and the failure that the team intends to prevent. Map the current workflow before changing it.
In the case of a manufacturer inspecting small surface defects on a moving production line, a change may help one group while harming another. The manufacturing quality team needs segmented results and a written acceptance rule. The strongest design makes its limitations visible before they become customer-facing incidents.
Handle calibration changes, shadow testing and model drift
In practice, handle calibration changes, shadow testing and model drift should be translated into an observable business decision, not treated as a feature that is complete once the software is installed. Map the current workflow before changing it.
Consider a manufacturer inspecting small surface defects on a moving production line. Instead of judging success by a demonstration, the manufacturing quality team should reproduce realistic cases, record exceptions, and compare the outcome against the current process. A simple decision log is often more useful than an elaborate dashboard because it connects evidence to an action.
What to do next: The manufacturing quality team should turn this part of the plan into a short written test, with an owner, an expected result, and a reason to revisit the decision. This is especially valuable when a pilot is handed to a separate production team.
Business case and implementation phases
Evaluate throughput, scrap reduction, inspection labor and downtime
In practice, throughput, scrap reduction, inspection labor and downtime should be translated into an observable business decision, not treated as a feature that is complete once the software is installed. Map the current workflow before changing it.
Consider a manufacturer inspecting small surface defects on a moving production line. Instead of judging success by a demonstration, the manufacturing quality team should reproduce realistic cases, record exceptions, and compare the outcome against the current process. A simple decision log is often more useful than an elaborate dashboard because it connects evidence to an action.
Propose pilot acceptance criteria and ongoing defect review
The useful question is not whether this capability exists in principle, but how the team will validate it under normal and exceptional conditions. Map the current workflow before changing it.
For example, with a manufacturer inspecting small surface defects on a moving production line, the first version can be evaluated on a small, representative sample. The manufacturing quality team should keep difficult cases in the test set rather than removing them because they make the results look worse. The goal is repeatable performance under stated conditions, not a claim that the technique eliminates uncertainty.
What to do next: The manufacturing quality team should turn this part of the plan into a short written test, with an owner, an expected result, and a reason to revisit the decision. This is especially valuable when a pilot is handed to a separate production team.
Practical Metrics and Implementation Priorities
Illustrative numbers: Consider 10,000 inspected products containing 200 confirmed defects. A system flags 240 items, including 180 true defects. Precision is 75% (180/240), while recall is 90% (180/200); those measures describe different trade-offs. These values are hypothetical worked examples, not published industry averages or evidence of a typical result.
Implementation priorities
- Choose thresholds based on the cost of missed defects.
- Measure false positives by product line and lighting.
- Inspect difficult edge cases under real factory conditions.
- Keep a traceable path for human override.
What to measure before scaling
- Baseline performance and clearly defined measurement period
- Result quality and important error categories
- Operational cost, review workload and downstream impact
- Changes in metrics across customer segments and scenarios
FAQ:
1. How does AI defect detection work?
Cameras capture production images and models flag visual patterns associated with defects. Reliable systems also need controlled lighting, traceability and a defined reject process.
2. What defects can computer vision detect?
Common examples include scratches, missing components, incorrect labels, surface contamination and dimensional anomalies visible in the image. Hidden structural faults need other sensors or tests.
3. How much training data is necessary?
There is no universal minimum. Requirements depend on defect variety, lighting and product consistency; rare defects may need anomaly-detection approaches and carefully reviewed samples.
4. How do manufacturers reduce false rejects?
Tune thresholds on realistic line data and separate borderline cases for operator review. Evaluate false positives and missed defects by defect type.
5. Does changing lighting affect model accuracy?
Yes. Reflection, shadow and color shifts can be mistaken for defects. Standardize illumination and test across expected operating conditions.
6. Can quality-control AI run at the edge?
Often yes, particularly when inspection requires low latency or local processing. Hardware selection depends on frame rate, model size and camera resolution.
7. How should inspection results be audited?
Keep image references, model versions, decision timestamps and operator overrides under an appropriate retention policy. This helps investigate recurring quality problems.
8. What are the key performance metrics?
Track defect recall, precision, false reject rate, throughput and latency. Measure results separately for critical defect classes.
9. Can one model inspect every product line?
Usually not without adaptation. Different surfaces, viewpoints and defect taxonomies can require different cameras, rules or models.
10. What is a sensible first deployment?
Choose one visually consistent inspection point and compare AI findings with verified human judgments over several production shifts.
Key Takeaways
The best next step is to select a bounded use case, document the present workflow, and agree on the evidence that would justify expansion. For AI visual inspection, measure outcomes that matter to users as well as technical indicators. Keep a human accountable for exceptions, and review results after the real operating environment changes.
Practical Implementation Checklist
Begin by documenting the decision this technology is meant to support. For a manufacturer inspecting small surface defects on a moving production line, specify what users submit, what they expect back, and which outcomes count as success. Keep the first test small enough to diagnose; do not begin with a company-wide rollout simply because the prototype looks promising.